High-Assay Botanical Extracts & Specialty Food-Grade Ingredients
Engineered for high bioavailability, chemical stability, and rigorous batch repeatability across industrial dietary, food-fortification, and formulation pipelines.
Cosmetic Raw Material Acetyl Tetrapeptide-2 Powder Bulk CAS 757966-65-7 Acetyl Tetrapeptide-2 Powder
20 Factory Supply Polysorbate 20 Cosmetic Grade Polysorbate 20 Liquid
High Quality 99% Hydroxypinacolone Retinoate CAS 893412-73-2 HPR Powder Hydroxypinacolone Retinoate
Factory Bulk Price Cas 11006-56-7 Food Grade Pangamic Acid Vitamin B15 Powder
Hot Sale Cosmetic Ingredient Tranexamic Acid Powder TXA White Powder CAS 1197-18-8
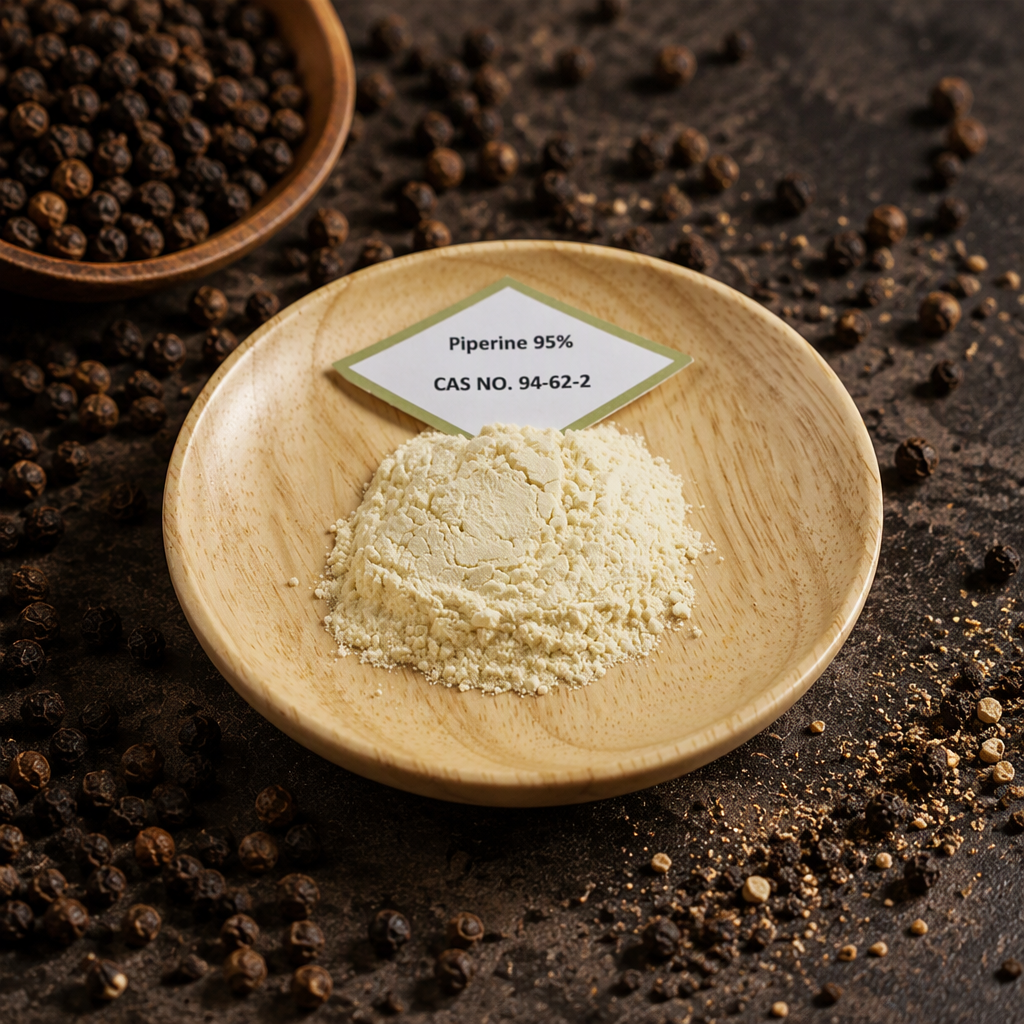
Factory Hot-Selling Black Pepper Extract Powder 95% 98% Piperine
Food Grade L Tyrosine Powder CAS 60-18-4 Pure L-Tyrosine
High Quality Hydrolyzed Rice Protein Powder Rice Protein 90%
Localized Applications Across Chongjin’s Manufacturing Landscape
As the primary industrial port and marine-logistics gateway in North Hamgyong, Chongjin demands food-grade ingredients that withstand specific regional processing parameters, including thermal retort stability, shelf-life preservation under marine atmospheric conditions, and enzymatic synergy.
1. Marine Harvest & Seafood Food Preservation
Chongjin’s established seafood processing sector utilizes standardized botanical polyphenols and high-potency Piperine 95%-98% alongside food-grade ascorbic derivatives to retard lipid peroxidation in cold-water pelagic species (such as Alaska pollock, squid, and regional mackerel). Standardized plant extracts suppress trimethylamine formation and microbial rancidity, functioning as natural clean-label alternatives to synthetic BHT/BHA during commercial freezing, canning, and blast-chilling processes.
2. High-Protein Formulations & Grain Enrichment
Regional grain and starch manufacturing centers in North Hamgyong increasingly fortify staples with Hydrolyzed Rice Protein 90% and pure fermented L-Tyrosine (CAS 60-18-4). Hydrolyzed rice peptides exhibit an optimal Protein Digestibility Corrected Amino Acid Score (PDCAAS), offering hypoallergenic, low-viscosity reconstitution that integrates smoothly into commercial noodles, extruded biscuits, and localized emergency nutrient rations without altering paste rheology or gelatinization profiles.
3. Industrial Fermentation & Bio-Nutrient Substrates
In municipal fermentation, brewing, and vinegar fermentation plants across Chongjin, precision-refined plant extracts and enzymatic hydrolysates deliver critical non-protein nitrogen, micronutrient cofactors, and Pangamic Acid (Vitamin B15). These functional matrices dramatically accelerate biomass propagation rates in continuous culture fermenters, improving ethanol yield consistency and resistance to osmotic cellular shock during seasonal sub-zero processing cycles.
Emerging Procurement Trends & Phytochemical Standards in Chongjin
Purchasing authorities and enterprise plant directors in Chongjin are rapidly shifting from unstandardized crude herbals to analytically audited, HPLC-fingerprinted active extracts characterized by strict solvent-residue clearances and standardized mesh densities.
Transition to Quantitative Marker Verification
Procurement contracts across North Hamgyong now mandate verifiable Certificates of Analysis (COA) specifying exact active percentages via High-Performance Liquid Chromatography (HPLC) and Liquid Chromatography-Mass Spectrometry (LC-MS), eliminating non-standardized native decoctions.
Demanding Supercritical & Aqueous Extraction
To satisfy non-toxic industrial consumer profiles, food manufacturers in Chongjin specify ingredients processed without carcinogenic class-1 or class-2 organic solvents, mandating supercritical CO2, food-grade USP ethanol, or membrane filtration systems.
Hermetic, Cold-Climate Barrier Packaging
Due to the humid maritime climate of Chongjin’s bay followed by bitter freezing winters, factory buyers require moisture-proof, double-layer food-grade poly-foil lined vacuum packaging with oxygen-barrier integrity to prevent hygroscopic clumping during sea cargo transit.
Cross-Dock Direct Logistics Protocols
Factory purchasing teams favor Chinese primary manufacturers located in strategic export corridors who hold direct accounts with tier-1 international freight hubs, delivering guaranteed 3-5 day cross-border dispatch and full customs-bonded transit documents.
Standardized Specification Matrix & Pharmacopeial Clearances
Every industrial lot manufactured for cross-border export is released under exhaustive analytical screening, conforming to United States Pharmacopeia (USP), European Pharmacopoeia (EP), and Food Chemicals Codex (FCC) benchmarks.
| Ingredient Nomenclature | Assay Target (Active Marker) | CAS Identifier | Primary Assay Method | Heavy Metals (Pb/As/Cd/Hg) | Microbiological Standard | Standard Packaging |
|---|---|---|---|---|---|---|
| Black Pepper Extract | ≥ 95.0% - 98.0% Piperine | 94-62-2 | HPLC Reverse-Phase | ≤ 10.0 ppm Total (ICP-MS) | Total Plate Count < 1,000 cfu/g | 25 kg / Fiber Drum (Foil Lined) |
| Hydrolyzed Rice Protein | ≥ 90.0% Protein (Dry Basis) | 94350-05-7 | Kjeldahl Digestion (N × 6.25) | ≤ 5.0 ppm Total | Salmonella / E. coli Absent | 20 kg / Multi-Wall Kraft Bag |
| Food Grade L-Tyrosine | ≥ 99.0% - 101.0% Pure | 60-18-4 | Potentiometric Titration | ≤ 10.0 ppm (Pb ≤ 2.0 ppm) | Yeasts & Molds < 100 cfu/g | 25 kg / Moisture-Proof Drum |
| Pangamic Acid (Vit B15) | Food Grade Assay Benchmark | 11006-56-7 | UV-Vis / Ion-Exchange | ≤ 10.0 ppm Total | Coliforms < 10 cfu/g | 25 kg / Aseptic Sealed Drum |
| Tranexamic Acid (TXA) | ≥ 99.0% Pure Crystalline | 1197-18-8 | HPLC / Acidimetric Titration | ≤ 5.0 ppm Total | Microbial Limit Compliant | 1 kg Foil Pouch / 25 kg Drum |
| Polysorbate 20 Liquid | FCC / USP Compliant Emulsifier | 9005-64-5 | Saponification / Hydroxyl Value | ≤ 2.0 ppm Heavy Metals | Bioburden Validated | 25 kg / 200 kg HDPE Sealed Drum |
Why Tier-1 Regional Processors Partner with Gavra Bio-Tech
Operating a vertically integrated extraction infrastructure in Henan, China, Gavra Bio-Tech Co.,Ltd. merges proprietary agricultural raw material cultivation with pharmaceutical-grade molecular separation lines.
Independent Analytical & Testing Center
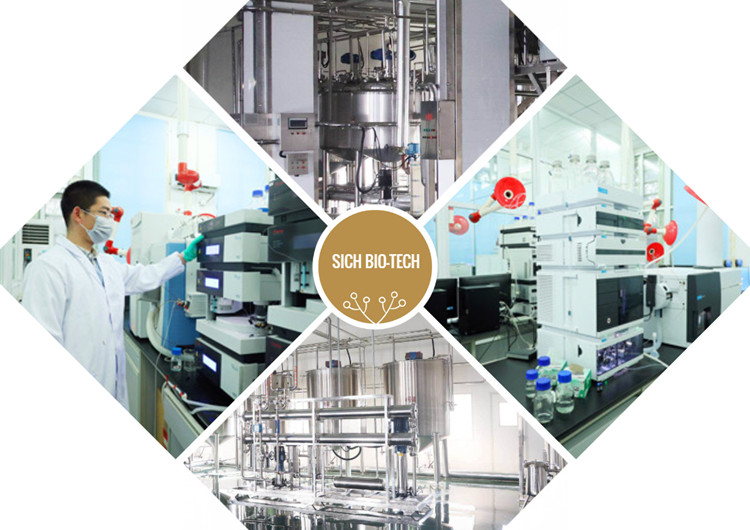
Our in-house QC laboratory houses precision instrumentation, including Waters LC-MS systems, Agilent 8453 UV-Vis spectrophotometers, and Swiss CAMAG High-Performance Thin-Layer Chromatography (HPTLC) scanners, guaranteeing that every export lot has quantifiable marker integrity, complete pesticide residue clearance, and low heavy metal profiles.
Multi-Stage Industrial Extraction Capacity
Our 8,000 m² GMP-compliant production workshop encompasses 3 automated extraction lines, continuous counter-current solid-liquid extractors, molecular distillation towers, column chromatography filtration, and closed-loop aseptic spray drying, processing over 1,200 metric tons of botanical biomass annually.
Direct SVIP Express Logistics & Ready Stock
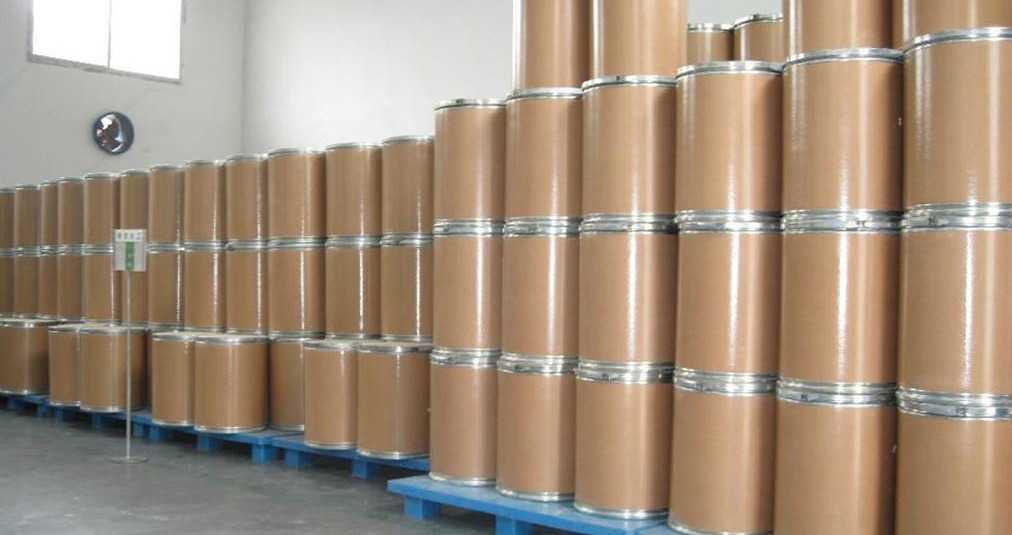
Holding top-tier SVIP commercial agreements with international logistics freight leaders, Gavra Bio-Tech provides Chongjin manufacturing buyers with streamlined door-to-port and bonded cross-border solutions. In-stock SKUs leave our warehouse within 3 to 5 business days, supported by comprehensive batch-specific COAs, MSDS, and non-GMO statements.
Frequently Asked Questions by Industrial Sourcing Teams in Chongjin
Clear, direct answers regarding testing validations, import compliance, lead-times, and custom botanical formulations.
What is the standard Minimum Order Quantity (MOQ) for plant extracts and nutritional powders?
How do you guarantee batch identity and verify the absence of adulteration or solvent residue?
Can food processing plants in Chongjin request custom mesh particle sizing and solubility optimization?
What shipping methods and documentation accompany cross-border shipments to Northeast Asian trade points?
Do you support contract OEM finished formats for dietary tablets, hard capsules, and functional gummies?
Are pre-shipment evaluation samples available prior to entering large volume industrial purchase agreements?
Connect with Our Phytochemical Technical Sourcing Team
Whether you are reformulating regional beverage profiles, scaling marine protein stabilization, or seeking stable food-grade botanical supplies in Chongjin, our formulation engineers provide comprehensive quotation dossiers, technical documentation, and pilot sample kits within 2 hours.