8,000 m²
GMP Workshop Surface
500 Acres
Traceable Botanical Fields
150+ Sets
Analytical & Extraction Gear
≤ 2 Hours
Average Spec Response Time
Primary Sourced Extracts & Active Ingredients
Lab-verified raw materials and functional ingredients available for immediate dispatch, industrial manufacturing, and private labeling.
Technical Whitepaper: Industrial Herbal Extract Processing & Supply Chain Mechanics
The manufacturing of commercial-grade nutraceutical extracts has evolved beyond basic maceration and solvent washing. Contemporary biopharmaceutical and functional nutrition brands require standardized botanical active fractions with guaranteed molecule density, batch homogeneity, and uncompromising documentation. As regulatory oversight across North America and global trading corridors tightens under cGMP (21 CFR Part 111) and ISO 22000 paradigms, direct-to-factory sourcing represents the most defensible risk-mitigation strategy for procurement executives.
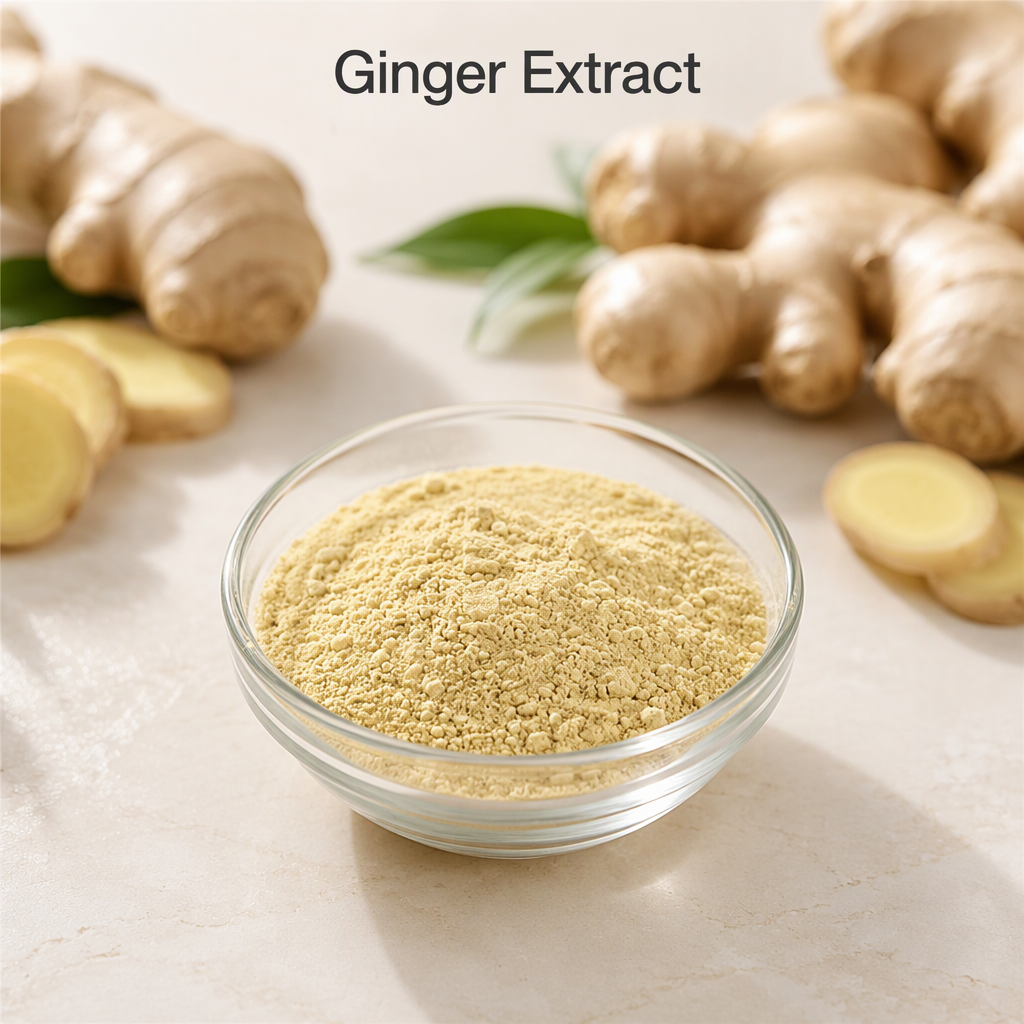
Industrial extraction protocols necessitate granular control over solvent-to-feedstock ratios, targeted thermal exposure thresholds to prevent active thermolability, and supercritical extraction dynamics. At Gavra Bio-Tech, our industrial workshops utilize continuous countercurrent extraction, specialized molecular distillation, and industrial-scale column chromatography. This multi-tiered processing topology enables the precise isolation of sensitive compounds—such as the volatile gingerols and shogaols found in premium ginger extracts, or the complex polysaccharide matrices of Poria Cocos—while stripping away trace residual solvents and heavy metal contaminants.
"Quality by Design (QbD) in herbal extraction ensures that critical quality attributes (CQAs)—such as particle mesh dynamics, hygroscopicity, botanical fingerprint consistency, and active compound assays—are engineered systematically into the manufacturing cycle rather than tested as an afterthought."
The logistical interface between bulk chemical synthesizers, botanical cultivation bases, and end-market regional distribution hubs like Grenville highlights an operational imperative: cross-border chemical transparency. A compliant supply model relies on verifiable HPLC (High-Performance Liquid Chromatography) assay baselines, LC-MS compound confirmation, and verified Certificates of Analysis (COA) matching lot numbers directly back to cleanroom bulk packaging.
| Functional Category | Core Analytical Metric | Extraction Mechanism | Industrial Formulation Target |
|---|---|---|---|
| Standardized Herbal Solids (e.g., Ginger, Red Clover) | Assay percentage (HPLC/UV) | Supercritical CO₂ / Ethanolic Reflux | Digestive tablets, systemic circulation capsules |
| Polysaccharide Complexes (e.g., Poria Cocos, Wild Jujube) | Total Polysaccharide content (UV-Vis) | Aqueous thermal extraction & ethanol precipitation | Immunomodulatory tinctures, meal replacement powders |
| Pure Cosmeceuticals & Peptides (e.g., HPR, Ectoine, GHK-Cu) | Isomer validation & Purity (LC-MS) | Biotechnological synthesis & crystallization | Targeted barrier repair, micro-emulsions, anti-wrinkle serums |
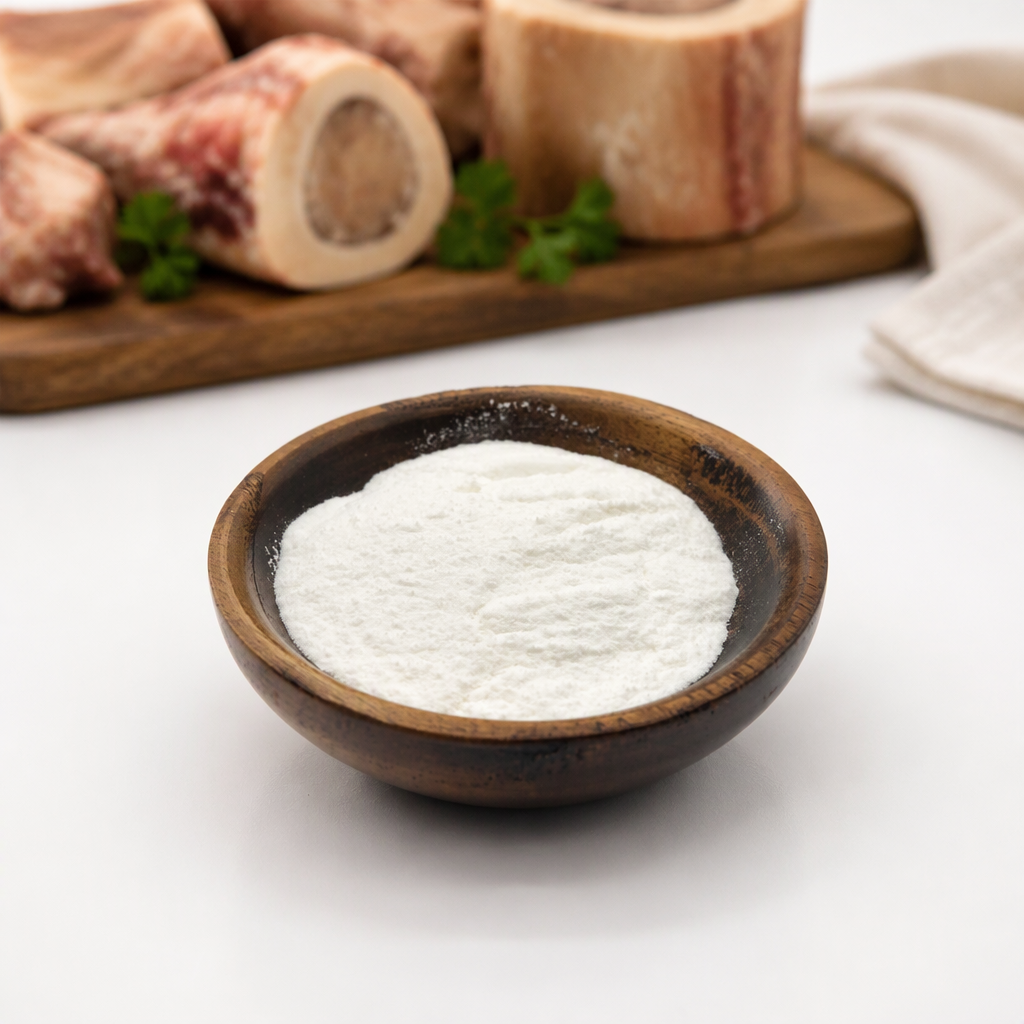
| Bioactive Structural Peptides (Bovine Marrow) | Molecular weight distribution (<1000 Da) | Controlled Enzymatic Hydrolysis | Connective tissue functional nutrition, clinical foods |
Localized Application Scenarios in Grenville Industrial & Commercial Ecosystems
Grenville's strategic positioning within regional logistics, agricultural distribution, and emerging wellness manufacturing creates diverse use cases for high-grade botanical extracts, bulk amino acids, and high-purity biological actives. Sourcing directly from certified facilities allows localized operations to develop cost-competitive product lines that fulfill specific market demands:
- Commercial Livestock & Agricultural Blends: Integrating bulk Feed Grade L-Threonine (CAS 72-19-5) into regional livestock feeds optimizes crude protein efficiency, mitigates nitrogenous waste, and enhances gut immunity across regional commercial animal husbandry networks.
- Specialty Beverage & Functional Botanical Infusions: Standardized Ginger Extract (yielding verifiable gingerols) and water-dispersible Poria Cocos polysaccharides serve regional contract packagers producing shelf-stable health beverages, wellness shots, and digestive tonics customized for regional taste profiles.
- Dermaceutical & Topical Barrier Formulations: Regional compounding pharmacies and boutique personal care laboratories incorporate Ectoine (99% HPLC) and Hydroxypinacolone Retinoate (HPR). These ingredients offer thermal and UV stress resistance alongside cellular regeneration properties, forming the foundation of protective daily skincare suited to diverse climatic conditions.
- Senior Nutrition & Clinical Recovery Blends: Bovine Bone Marrow Collagen Peptides combined with standard USP-grade Folic Acid allow contract manufacturing organizations (CMOs) to formulate bio-accessible powders aimed at joint support, mobility restoration, and systemic vitality.
Macro Industry Trends Shaping Grenville Procurement
The procurement parameters for active ingredients in the Grenville market are experiencing substantial structural changes driven by increased analytical scrutiny, supply chain decentralization, and clean-label end-user preferences:
- Transition to Single-Active Transparency: Formulators are steadily shifting away from non-standardized raw herbal powders toward quantified botanical extracts. Demands for standardized active assays (e.g., exact 5% to 20% Gingerol markers instead of arbitrary 4:1 ratios) ensure repeatable pharmacokinetics across consumer batches.
- Biotech Synergies (Green Synthesis & Fermentation): Natural extremolytes like Ectoine and biological peptides are transitioning from high-cost niche imports to staple formulation inputs. Local manufacturers are combining traditional botanical extracts with fermentation-derived actives to produce multi-action cosmeceutical lines.
- Near-Zero Adulteration Tolerance: Regional regulatory authorities and quality control divisions have upgraded chromatographic auditing. Screening for synthetic adulterants, undeclared carrier starches, and heavy metal concentrations (Lead, Arsenic, Cadmium, Mercury) has made factory-level LC-MS and HPTLC documentation a prerequisite for entry.
- Flexible Batch Aggregation (Low MOQs with Industrial Pricing): Emerging brands in the region are adopting lean inventory strategies. By partnering with direct manufacturers that provide 1 kg to 25 kg starter allotments alongside rapid 3–5 day dispatch windows, regional producers lower cash exposure while securing bulk pricing structures.
Enterprise Strengths & Analytical Infrastructure
Gavra Bio-Tech connects raw botanical cultivation to finished analytical testing, providing industrial buyers with audited consistency.
500-Acre Traceable Fields
Direct ownership of botanical cultivation fields ensures that biomass is harvested at physiological maturity, free from industrial pesticides, and entirely traceable from soil bed to loading dock.
8,000 m² cGMP Workshop
Equipped with 3 specialized production lines handling complex extraction, vacuum distillation, precision rectification, and preparative chromatography under controlled cleanroom air standards.
In-House Analytical Verification
Our dedicated quality control labs utilize Waters LC-MS, Agilent 8453 UV-Vis spectrophotometers, and Swiss HPTLC systems to eliminate out-of-specification deliveries before departure.
Full OEM Finished Formats
Beyond raw powder distribution, our facility supports full contract manufacturing of chewable gummies, two-piece hard gelatin/HPMC capsules, and compressed tablets formulated to buyer requirements.
FedEx & DHL SVIP Logistics
Optimized freight workflows and priority booking ensure warehouse dispatch within 3–5 working days post-settlement, offering international buyers full DDP, CIF, and FOB transparency.
Technical Sales Engineering
Our technical team responds within 2 hours with real-time inventory confirmations, full third-party test data packages, and formulation compatibility advice.
Waters LC-MS Chromatography
Molecular Weight Confirmation & Impurity Profiling8453 UV-Vis Spectrophotometer
Standardized Active Potency & Absorbance ValidationSwiss HPTLC Scanner
Botanical Fingerprinting & Adulteration ScreeningProcurement & Compliance FAQ for Grenville Buyers
Addressing the technical, regulatory, and logistics inquiries commonly raised during commercial qualification.
What are the minimum order quantities (MOQ) for pilot runs?
For standardized herbal extracts, food-grade additives, and common vitamins, our MOQ begins at 1 kg. Highly active cosmetic peptides start from 1 g to 10 g, while select industrial commodities (e.g., bulk sweeteners or raw carrier powders) are supplied in standard 25 kg multi-wall fiber drums.
Are free pilot evaluation samples provided to formulators?
Yes. We provide complimentary laboratory-scale samples (typically 20 g to 50 g) to qualified corporate formulators and production centers for sensory evaluation, analytical re-testing, and pilot formulation trials. Courier shipping arrangements can be scheduled instantly via live chat.
What documentation accompanies commercial botanical shipments?
Every lot is shipped with a fully traceable Certificate of Analysis (COA) detailing active assay percentages, moisture loss, total ash, residual solvents, microbiological counts (aerobic plate count, yeast/mold, E. coli, Salmonella), and heavy metal tests (ICP-MS). MSDS, Flow Charts, and TSE/BSE declarations are provided upon request.
What are the expected transit times and clearance protocols?
In-stock inventory is packaged and dispatched from our primary warehouse within 3 to 5 business days after invoice confirmation. As an SVIP shipper with DHL and FedEx, transit typically averages 4 to 7 business days for express freight, while standard air and maritime freight solutions are available under DDP, CIF, and FOB terms.
Can you provide customized particle mesh sizes or carrier-free extracts?
Yes. Our processing lines can adjust particle sizing from 80-mesh standard powders down to micronized 200-mesh parameters for rapid dissolution profiles. Additionally, we produce carrier-free extracts or utilize pure organic maltodextrin/rice flour carriers based entirely on the technical parameters of your manufacturing equipment.
How are temperature-sensitive actives packaged for international transit?
Thermally sensitive products (such as bioactive peptides, pure liquid panthenol, or stabilized cosmetic retinoids) are packaged inside double-lined vacuum-sealed medical-grade LDPE pouches enclosed within light-blocking multi-layer aluminum foil containers, accompanied by desiccant inserts and cold packs when appropriate.
Request Technical Dossiers, Batch Samples, or Factory Pricing
Consult directly with our on-duty analytical sales engineers. Receive comprehensive COAs, custom manufacturing timelines, and quotation structures customized for your project scale.
Get a Quote